
How automotive PCB assembly processes prevent solder joint failures
DETAILS
A solder joint in an automotive electronic assembly rarely fails because of one isolated defect. Cracking, opens, intermittent resistance, and solder fatigue usually emerge from a chain of decisions made before and during production: the footprint geometry, board finish, component storage, paste deposition, placement accuracy, reflow profile, cleaning strategy, and validation method.
That is why a capable PCB assembly process automotive program should be evaluated as a controlled system rather than as a list of inspection machines. An assembly may look acceptable after reflow and still contain joints that are vulnerable to vibration, repeated thermal expansion, moisture exposure, or long service life. The practical question is whether the manufacturing process creates stable solder joints consistently, and whether it can demonstrate that stability for the actual vehicle environment.
Solder failures begin with mechanical and thermal mismatch
Automotive electronics place solder joints under stresses that are less forgiving than those in many indoor applications. A control module near a powertrain, an underbody sensor, a battery-management board, and an in-cabin infotainment controller may all use similar soldering methods, but their exposure conditions are very different.
The board laminate, copper structure, package body, component termination, and solder alloy expand at different rates as temperature changes. Each heating and cooling cycle transfers strain into the solder joint. Vibration adds cyclic mechanical loading. Large components, heavy connectors, leadless packages with bottom-side terminations, and parts mounted near board edges can concentrate that strain further.
A process cannot eliminate every source of stress. It can prevent manufacturing conditions from adding avoidable weakness. Poor wetting, insufficient solder volume, voids in thermal joints, disturbed joints during cooling, pad damage, or marginal component coplanarity all reduce the amount of stress a joint can tolerate. The assembly objective is therefore not merely “good solder appearance.” It is a repeatable metallurgical bond with sufficient geometry and process margin for its use condition.
Design-for-assembly controls determine whether the line has a reliable process window
Manufacturing prevention starts before solder paste reaches the PCB. A technically sound design can still become difficult to assemble when the land pattern, solder mask opening, pad finish, and component package requirements are not reviewed as one system.
For fine-pitch and bottom-terminated devices, the pad geometry directly influences solder volume and collapse behavior during reflow. Excess paste can promote bridging, floating, or excessive voiding. Too little paste can create incomplete joints or leave insufficient fatigue margin. Thermal pads require particular care: a single large stencil opening can deposit more paste than the joint can vent during reflow, increasing the likelihood of voids or package float. Segmented aperture designs are commonly used to manage paste transfer and outgassing while maintaining thermal and mechanical contact.
Board surface finish is another process input, not a cosmetic detail. It affects solderability, storage behavior, and the stability of the wetting process. The selected finish must suit the component terminations, assembly sequence, expected storage conditions, and any later rework requirements. A supplier should be able to explain how incoming board finish condition is checked and how boards with oxidation, contamination, warpage, or damaged pads are handled.
Technical evaluators should also examine component packaging and moisture handling. Some packages are sensitive to absorbed moisture during reflow. Inadequate dry storage, uncontrolled floor life, or incorrect bake handling can damage package integrity and create latent reliability risks. This is especially relevant when component supply comes from multiple sources or when production schedules leave partially used reels exposed on the shop floor.
Stencil printing is where solder-joint consistency is won or lost
Reflow cannot correct a poorly controlled paste deposit. The printing stage determines the initial solder volume and placement on each pad, so it has a disproportionate influence on open joints, bridges, insufficient fillets, and inconsistent thermal-pad connections.
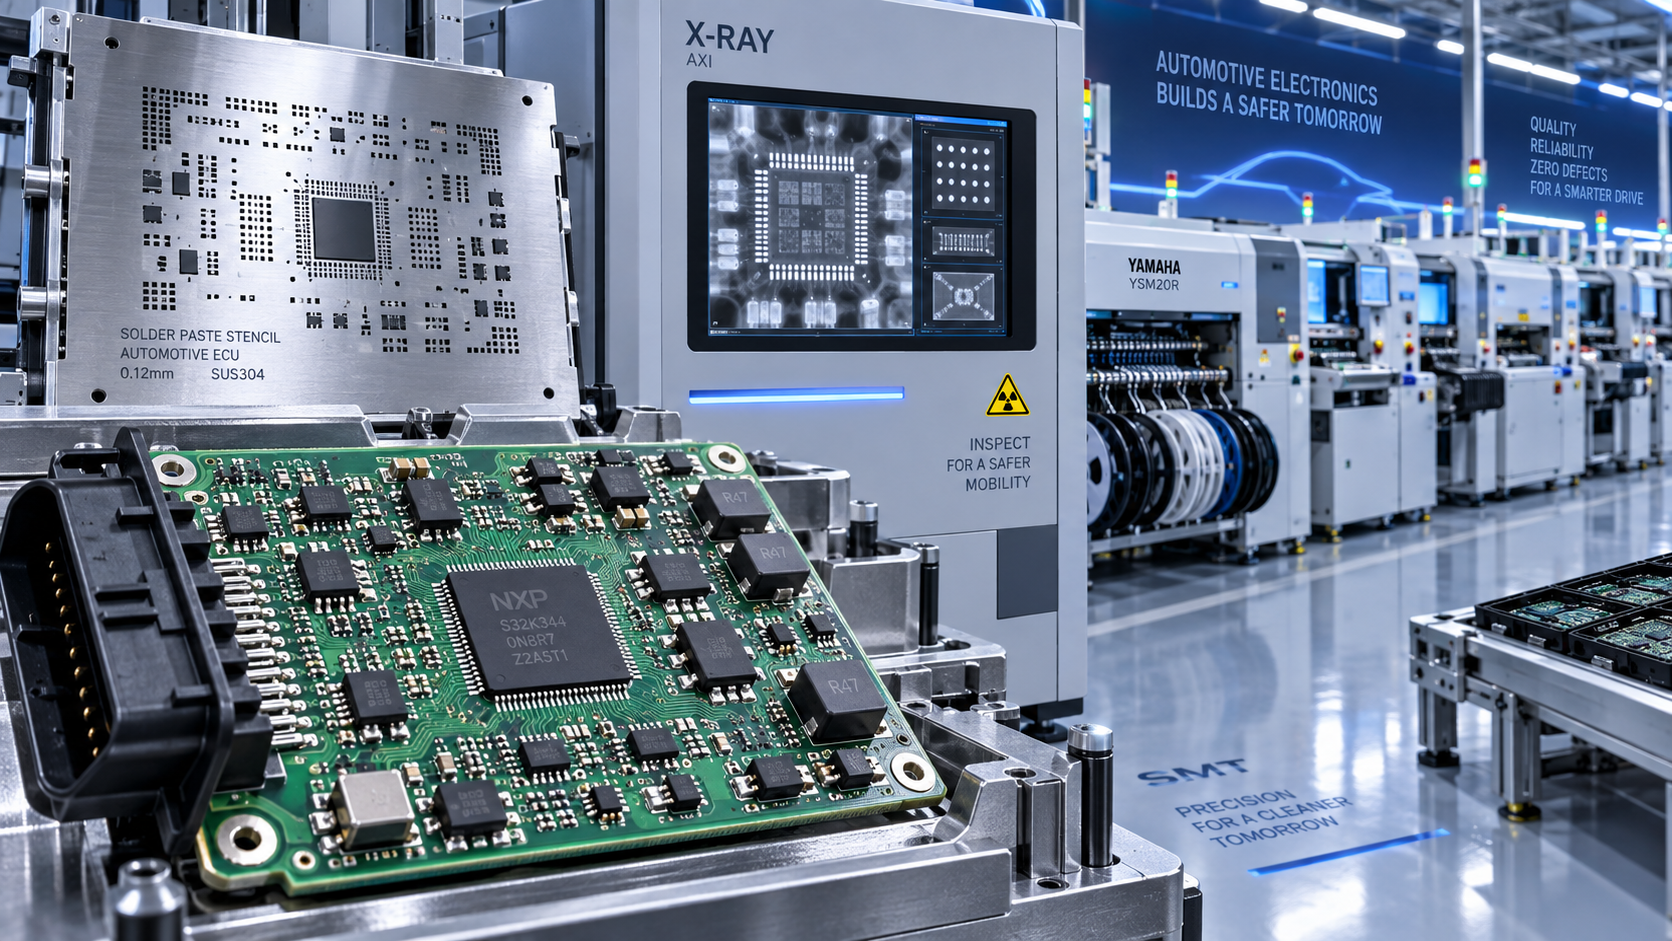
A robust SMT assembly process controls more than nominal stencil thickness. It verifies aperture design, paste condition, squeegee performance, board support, alignment, print pressure, separation behavior, and cleaning frequency. The important evidence is not that a stencil printer exists, but that the manufacturer measures deposits and responds to trends before defects become visible at final inspection.
Solder paste inspection is particularly valuable for components whose joints cannot be fully viewed after placement. If paste height, area, or volume drifts on a QFN, BGA, power package, or connector footprint, the defect may remain hidden until electrical test, X-ray inspection, or field use. Process data should connect paste measurement to the relevant component families and acceptance limits, rather than treating all pads as equivalent.
Why “within average” is not enough
Average paste volume can conceal unstable printing. A board may meet an overall average while a small group of critical pads repeatedly receives marginal deposits. For automotive assemblies, review should focus on distribution, repeatability, and outlier management around high-risk joints: power-device thermal pads, large ceramic capacitors, fine-pitch connectors, bottom-terminated packages, and components exposed to board flex.
Placement accuracy protects the intended solder geometry
Modern placement equipment can achieve high accuracy, but the evaluated capability should include the entire placement chain: feeder condition, vision recognition, nozzle selection, component centering, board fiducials, support tooling, and handling of odd-form parts. A placement offset that appears minor can turn a correctly printed deposit into an off-center or partially wetted joint.
Component coplanarity deserves attention where leadless packages, large passive components, or power devices are involved. A package that does not sit evenly on the deposited paste may create uneven joints, insufficient contact on one termination, or lifted corners after reflow. The line should have a defined response when incoming component variation exceeds the placement process capability.
Board support also matters. If the PCB bends during placement or reflow, solder volumes and component contact can change across the panel. Large panels, thin boards, high-mass parts, and dense assemblies often need carefully positioned tooling support. This is a practical example of why placement accuracy specifications alone do not establish solder-joint reliability.
Reflow profiling must be tied to the actual board, not a generic recipe
A reflow profile is the thermal history experienced by the assembly. It must bring every relevant joint through the required melting and wetting stages without overheating temperature-sensitive components, degrading board materials, or creating excessive thermal gradients.
Automotive boards are rarely thermally uniform. Copper planes, heavy power sections, shields, connectors, dense fine-pitch areas, and large heat-spreading pads absorb and release heat differently. A profile that works for a lightly populated control board may leave joints on a high-copper power board underheated, while overheating smaller components elsewhere.
The reflow study should use representative assemblies and measure locations with distinctly different thermal mass. It should account for the specified solder alloy, paste supplier guidance, component temperature limits, oven loading, conveyor speed, and board orientation. Profile control must continue after initial setup; changes in board stack-up, copper balance, component mix, oven maintenance, or throughput can alter the thermal result.
One common mistake is treating peak temperature as the sole indicator of reflow quality. Wetting behavior depends on the full profile, including ramp rate, time in the activation range, time above liquidus, and cooling behavior. A joint can reach an acceptable peak and still have poor wetting or undesirable microstructure because other parts of the profile were not controlled.
Inspection should be risk-based, not limited to visible defects
Automated optical inspection is useful for polarity, component presence, placement offset, visible solder bridges, and many leaded-joint defects. It cannot fully assess hidden solder interfaces beneath BGAs, QFNs, land-grid packages, or large thermal pads. A process that relies only on visual inspection may pass assemblies with concealed opens, insufficient solder, or voiding patterns that matter for thermal and mechanical reliability.
The right inspection mix depends on the assembly’s risk profile. Hidden solder joints, high-current paths, thermal interfaces, safety-relevant circuits, and mechanically loaded connectors justify more targeted process verification than simple low-risk boards. X-ray should not be treated as an automatic guarantee, either. Its value depends on component-specific criteria, sampling logic, image quality, and documented action when trends drift.
Cleaning, handling, and rework can create failures after the main soldering step
Residues, contamination, and handling damage are often underestimated because they may not produce an immediate electrical failure. Flux residues can be acceptable only when they are compatible with the operating environment and the process is controlled. In humid or contaminated service conditions, residue behavior, ionic contamination, and insufficient cleaning can contribute to leakage or corrosion risks. The question is not whether a line uses a no-clean material or a wash process; it is whether that choice is validated for the assembly, materials, and environment.
Rework needs equally strict discipline. Local heating can affect nearby components, pads, laminate adhesion, and adjacent solder joints. Repeated rework is especially concerning on fine-pitch devices, thermally demanding packages, and boards with heavy copper. A credible process records rework causes, limits repeated thermal exposure, verifies the repaired joint with an appropriate inspection method, and uses recurring rework data to correct the upstream source of the defect.
Reliability validation must reflect the failure mechanism being controlled
End-of-line testing demonstrates that a unit works at that moment. It does not, by itself, demonstrate resistance to repeated expansion, vibration, moisture, or mechanical shock. Reliability qualification should be selected according to the realistic failure mechanism. Thermal cycling is relevant where differential expansion drives solder fatigue. Vibration and mechanical shock matter where board flex, component mass, or mounting arrangement loads joints. Humidity-related evaluation is relevant when residues, coatings, exposed conductors, or enclosure conditions create moisture sensitivity.
It is also important to distinguish assembly-level qualification from generic material claims. A solder paste, laminate, coating, or component may have relevant documentation, but the final result depends on their interaction in the finished board. Changes in a component source, PCB fabricator, surface finish, solder paste, stencil, oven, or panel layout should be assessed for whether they alter the established process window.
What to request when assessing an automotive assembly supplier
A supplier comparison becomes more meaningful when it asks for evidence of process control rather than broad statements about automotive capability. The following items expose whether solder-joint prevention is embedded in normal production:
- Documented design-for-manufacturability review focused on critical packages, thermal pads, connectors, board flex, and solder-mask constraints.
- Component and PCB incoming inspection criteria, including traceability and controls for storage-sensitive materials.
- Stencil aperture rationale and paste-inspection records for high-risk component families.
- Representative reflow profile records tied to actual board construction and component thermal mass.
- Defined use of optical inspection, X-ray, electrical test, and destructive analysis for concealed or high-consequence joints.
- Clear defect escalation, root-cause analysis, corrective-action verification, and change-control practices.
- Reliability validation aligned with the intended temperature, vibration, moisture, and power-loading conditions.
Independent technical benchmarks can help procurement and engineering teams compare this evidence across suppliers. SiliconCore Metrics publishes analysis covering PCB materials, SMT placement precision, component reliability under environmental stress, and manufacturing compliance evidence. That kind of normalized technical review is most useful when it supports a defined engineering question, such as whether a supplier’s paste-volume control, reflow capability, or inspection coverage matches the assembly’s actual risk points.
The strongest prevention strategy is not a final inspection gate that catches obvious defects. It is a linked manufacturing system in which board design, materials, paste printing, placement, thermal processing, inspection, and reliability verification all protect the same solder joints. For an evaluator, the most revealing question is simple: when a critical joint is hidden, highly stressed, or difficult to rework, what process evidence shows that its reliability was designed and controlled before the product left the line?
Recommended News
- Reflow SolderingHow to compare thermal profiles for reflow process benchmarkingImprove reflow process benchmarking by comparing thermal profiles, process windows, and repeatability. Discover how to evaluate ovens and suppliers with reliable, auditable data.
- Reflow SolderingHow thermal cycling reliability testing reveals solder joint fatigueThermal cycling reliability testing reveals solder joint fatigue through CTE mismatch, crack monitoring, and failure analysis—learn how to build more reliable electronics.
- Reflow SolderingHow automotive PCB assembly processes prevent solder joint failuresPCB assembly process automotive controls help prevent solder joint failures through DFM, paste inspection, precise reflow profiling, and risk-based validation. Learn proven reliability practices.
- Reflow SolderingWhat SMT process capability evidence is needed for AEC-Q100 projects?SMT process capability AEC Q100 evidence: learn the essential controls for reflow, MSL, solder-joint inspection, traceability, and automotive release.
- Reflow SolderingWhen does FR4 PCB assembly need tighter reflow temperature control?FR4 PCB assembly needs tighter reflow control when thermal mass, fine-pitch components, moisture, and reliability demands narrow the process window. Learn key profiling factors.
- Reflow SolderingWhat BGA defects reveal weak SMT process capabilitySMT process capability BGA insights: learn how BGA defects expose weak printing, placement, reflow, and inspection control—and what they mean for reliability, audits, and supplier risk.