
How thermal cycling reliability testing reveals solder joint fatigue
DETAILS
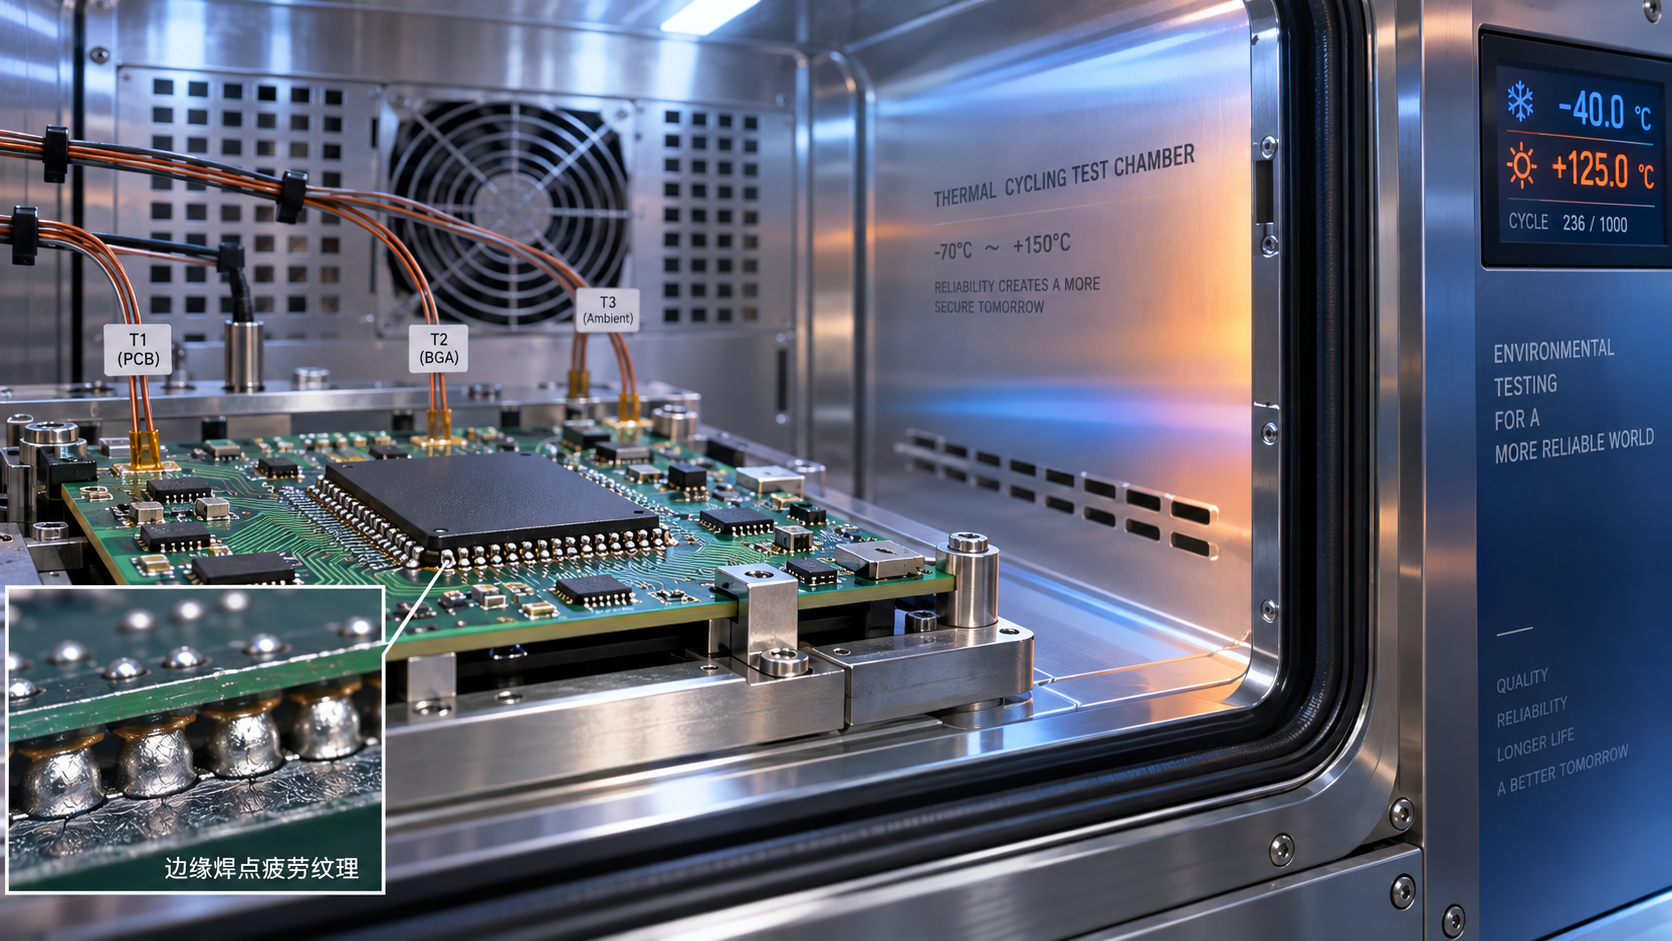
Thermal cycling reliability testing exposes solder joint fatigue by repeatedly forcing the assembly materials to expand and contract at different rates. A solder joint sits between materials with dissimilar coefficients of thermal expansion (CTE): a silicon die, package substrate, solder alloy, copper land, laminate, and sometimes a heatsink or mechanical support. Each temperature excursion produces strain. When that strain is repeated, local plastic deformation accumulates in the solder and damage begins at the locations where stress concentrates.
The value of the test is not simply that it creates failure. Its value is that the location, timing, and electrical signature of degradation reveal whether the weakness comes from package geometry, board construction, assembly conditions, component mass, solder volume, or the thermal profile imposed by the end application. A joint that remains electrically continuous during a short inspection can still contain an early fatigue crack. Thermal cycling, combined with appropriate monitoring and physical analysis, turns that hidden condition into observable evidence.
What the temperature cycle is actually loading
A temperature cycle is defined by more than its high and low setpoints. The dwell time at each extreme, transition rate, number of cycles, atmosphere, powered or unpowered state, fixture restraint, and temperature measurement location all influence the stress generated in the assembly. A rapid chamber air-temperature change is not automatically a rapid component-temperature change. Large packages, metal shields, thick copper regions, and thermally massive boards can lag the chamber considerably. If the test profile is qualified only by chamber air, the actual temperature swing at the soldered component may be smaller, delayed, or uneven.
During heating, the PCB and the package do not expand as a uniform body. The board expands most strongly in-plane, while a component package may expand less, more, or differently along each axis. At a ball grid array, the outermost joints are often subjected to greater shear displacement because the relative movement increases with distance from the package neutral point. At leaded packages, bending of the lead and local compliance can redistribute strain, although the lead-to-board interface may become the vulnerable region. Through-hole, press-fit, and connector structures introduce different load paths and cannot be interpreted using the same assumptions as fine-pitch surface-mount joints.
The solder itself changes response as temperature changes. At a higher portion of its melting temperature, solder becomes more susceptible to creep and stress relaxation. At lower temperatures, it can behave more stiffly and transfer stress differently into the intermetallic layer, pad finish, and package termination. A profile with long hot dwells can therefore reveal a different damage process from a cycle with the same nominal temperature range but brief dwells. Comparing cycle counts without comparing the full profile is a common source of false equivalence.
From cyclic strain to a detectable crack
Solder fatigue usually develops progressively rather than as a single sudden event. Repeated thermomechanical strain creates localized plastic deformation, often near a package-side interface, a board-side interface, a corner joint, or a region with reduced solder cross-section. Microstructural coarsening, grain-boundary sliding, voids, and growth of intermetallic compounds can reduce the joint's ability to accommodate further strain. A crack may then initiate and extend across the conductive path.
Electrical continuity monitoring is useful because an intermittent resistance increase often appears before a permanent open circuit. Yet continuity alone does not identify the failure mechanism. A resistance event that occurs only at the cold extreme may point to crack opening under contraction. A signal interruption during transition can result from dynamic board flexure, fixture vibration, or an unstable test connection rather than solder fatigue. A stable elevated resistance at room temperature after cycling suggests a more advanced structural change, but even then cross-sectioning or other physical analysis is needed before assigning root cause.
Cracks that look similar in an image may have different origins. A fracture through bulk solder can indicate accumulated thermal fatigue, while separation at an intermetallic interface may be associated with metallization condition, wetting quality, excessive intermetallic growth, or contamination. Pad cratering beneath the copper land is not a solder-joint fatigue failure, even though the electrical result can also be an open connection. It is commonly associated with board laminate weakness and mechanical bending or shock, but thermal cycling can worsen an existing crack or reveal a weak interface. The failure classification should follow the fracture path, not the electrical symptom alone.
Why joint geometry changes the result
Geometry controls both strain distribution and inspection visibility. A large BGA has a long distance from its center to its corner balls, so the outer rows deserve special attention. Package warpage can further alter the load: a component that is nearly flat at reflow temperature may warp as it cools, changing solder volume and joint shape across the array. The solder joints nearest the corners may be geometrically sound while joints in another region carry the greatest strain because of warpage-driven separation or compression.
Smaller components are not automatically less sensitive. Tiny chip resistors and capacitors have short stand-off heights, stiff terminations, and limited solder volume. Board bending near a rigid connector, screw boss, shield frame, or heat spreader can place their end terminations under concentrated stress. Large ceramic capacitors present a separate concern: flex cracking of the ceramic body may be mistaken for a solder defect if the test records a resistance change. The failure site must be established before changing the solder process.
Bottom-terminated components create another interpretation challenge. Their solder interfaces are hidden, and voiding beneath the termination may reduce the effective load-bearing area. Voids are not equivalent in every location. A void centered in a broad solder interface may have limited effect, while one located at a high-strain edge or joining with neighboring voids can accelerate crack initiation. X-ray images can reveal void patterns, but they do not directly show wetting quality, interface integrity, or fatigue crack direction.
Test parameters that should be read together
A thermal cycling report becomes meaningful when its parameters are tied to the expected service environment and the assembly construction. The following relationships are particularly important.
The low-temperature extreme deserves as much attention as the high-temperature extreme. Low-temperature contraction can increase tensile stress at interfaces and make marginal cracks electrically visible. High-temperature dwell can encourage solder creep and microstructural change. A test that uses only a high-temperature storage exposure assesses a different reliability question; it cannot substitute for cyclic thermomechanical loading.
Board construction must also be recorded. Copper distribution, laminate resin system, glass weave, thickness, layer count, plated-through-hole structure, and local stiffeners influence the board's expansion and warpage. Two boards with the same outline and component placement may produce different fatigue results when their copper balance or laminate properties differ. Treating the PCB as a passive carrier hides a major part of the load system.
Building evidence rather than collecting cycle counts
A useful test sequence begins with a defined failure criterion and an explicit measurement plan. Electrical daisy chains are often used to monitor a population of similar joints, but their routing and segmentation matter. A single chain across many joints can indicate that a discontinuity occurred without locating it. Segmented nets, redundant access points, or component-level measurements improve localization. The test circuit must withstand temperature movement without adding its own intermittent contacts through connectors, cable strain relief, or oxidized probe interfaces.
Pre-test characterization establishes the starting condition. This commonly includes visual inspection, electrical baseline measurements, solder paste and reflow records, X-ray review where hidden joints are involved, and dimensional confirmation of the assembled stack-up. Rework history requires particular scrutiny. Localized reheating can modify intermetallic thickness, solder microstructure, pad adhesion, and component warpage. A reworked assembly may survive initial functional testing yet behave differently under cycling from a first-pass production assembly.
Intermediate read points are often more informative than a single final inspection. A sudden cluster of failures following a particular interval can indicate a narrow fatigue distribution or a common process weakness. A gradual increase in intermittent events suggests progressive damage, although the measurement system must be checked before accepting that conclusion. Temperature-correlated resistance plots, event timestamps, and chamber records should be retained together. A failure detected at a given cycle is only meaningful when the actual part temperature and the measurement condition are known.
Physical failure analysis should preserve the evidence path. Cross-sectioning through an arbitrary location can miss a corner crack or create polishing damage that resembles a fracture. When feasible, non-destructive examination precedes destructive work. X-ray, acoustic methods, microsectioning, dye-and-pry methods, optical microscopy, and scanning electron microscopy each answer different questions. Dye penetration can show an opened interface, but it does not prove that the interface initiated the failure. A polished cross-section can reveal layer sequence and crack path, but it represents only one slice through a three-dimensional joint.
Separating thermal fatigue from test artifacts
Not every failure during cycling is caused by the temperature excursion. Fixture-induced bending can load the PCB at every transfer or clamp point. Cable movement can create electrical discontinuities. Condensation or contamination can distort leakage measurements near cold conditions. A board mounted with screws, rails, or heat sinks may be overconstrained in a way that differs sharply from its installed configuration. These factors are especially important when failures cluster near mounting points or appear on only one chamber position.
Replicate behavior provides context. If failures occur at similar joint locations across comparable samples, a design or process mechanism becomes more credible. If a lone assembly fails at an unusual location, review traceability, rework, handling history, and test setup before generalizing the result. The absence of failure also needs restraint in interpretation. Passing a chosen number of cycles means the tested population survived that profile and criterion; it does not establish immunity to other temperature ranges, vibration, board flexure, humidity, power cycling, or longer service exposure.
Using results in component and assembly qualification
Thermal cycling results become actionable when the tested configuration is fully traceable. The component revision, package finish, PCB fabrication lot, surface finish, solder alloy, paste type, stencil design, placement conditions, reflow profile, cleaning method, conformal coating status, and mechanical attachments can all affect the joint. A report that names only a component and a cycle count leaves too many variables unresolved for meaningful comparison.
When comparing two assembly sources, identical chamber setpoints are insufficient if board stack-up, solder paste, land pattern, reflow profile, or inspection threshold changed between builds. The comparison should distinguish a process qualification question from a design qualification question. If the goal is to evaluate assembly consistency, the design and materials need tight control. If the goal is to evaluate design robustness, deliberately varied builds can be useful, but the varied factors must be recorded and separated in the analysis.
The most defensible conclusion connects failure location, electrical behavior, temperature profile, and physical evidence. That connection identifies whether the next action belongs in package selection, pad design, PCB construction, assembly process control, mechanical mounting, or the test method itself. Thermal cycling reliability testing earns its value at that point: it converts repeated temperature exposure into a structured explanation of how a solder joint is accumulating fatigue before the same mechanism appears in service.
Recommended News
- Reflow SolderingHow to compare thermal profiles for reflow process benchmarkingImprove reflow process benchmarking by comparing thermal profiles, process windows, and repeatability. Discover how to evaluate ovens and suppliers with reliable, auditable data.
- Reflow SolderingHow thermal cycling reliability testing reveals solder joint fatigueThermal cycling reliability testing reveals solder joint fatigue through CTE mismatch, crack monitoring, and failure analysis—learn how to build more reliable electronics.
- Reflow SolderingHow automotive PCB assembly processes prevent solder joint failuresPCB assembly process automotive controls help prevent solder joint failures through DFM, paste inspection, precise reflow profiling, and risk-based validation. Learn proven reliability practices.
- Reflow SolderingWhat SMT process capability evidence is needed for AEC-Q100 projects?SMT process capability AEC Q100 evidence: learn the essential controls for reflow, MSL, solder-joint inspection, traceability, and automotive release.
- Reflow SolderingWhen does FR4 PCB assembly need tighter reflow temperature control?FR4 PCB assembly needs tighter reflow control when thermal mass, fine-pitch components, moisture, and reliability demands narrow the process window. Learn key profiling factors.
- Reflow SolderingWhat BGA defects reveal weak SMT process capabilitySMT process capability BGA insights: learn how BGA defects expose weak printing, placement, reflow, and inspection control—and what they mean for reliability, audits, and supplier risk.