
Which AOI inspection standards apply to PCB assembly quality control?
DETAILS
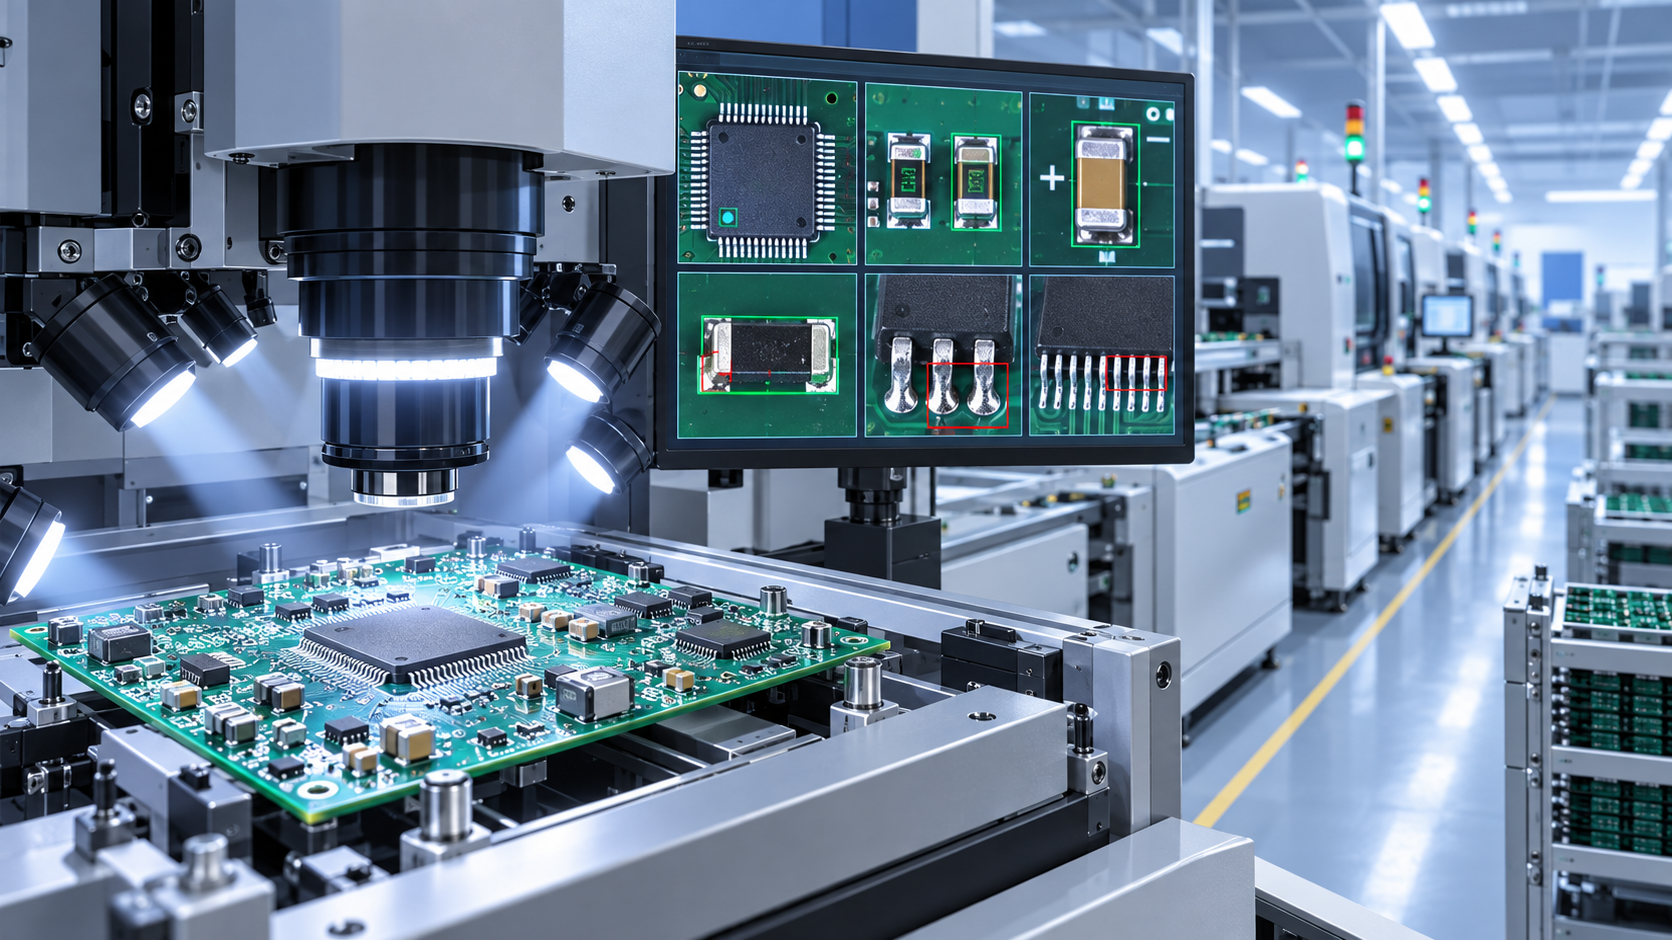
AOI inspection for PCB assembly is governed primarily by the acceptance requirements in IPC-A-610, supported by the soldering-process requirements in IPC J-STD-001. AOI equipment does not create a separate universal acceptance standard. It converts defined assembly criteria, approved component data, and process tolerances into repeatable optical rules. The inspection program is therefore only as valid as the standard, revision level, product class, and documented disposition rules behind it.
For assembled electronic products, IPC-A-610 is normally the central visual acceptance reference. It defines conditions that are acceptable, process indicators, or defects for soldered assemblies and mounted components. J-STD-001 complements it by defining requirements for soldered electrical and electronic assemblies, including workmanship conditions that influence solder-joint quality and reliability. AOI is effective for visible conditions within these requirements, but it cannot confirm every requirement covered by either document.
Standards that define AOI inspection criteria
IPC-A-610, Acceptability of Electronic Assemblies, is the main standard used to determine whether visible assembly conditions meet the required class of workmanship. AOI libraries and inspection recipes commonly translate its criteria into measurable checks for component presence, polarity, orientation, placement offset, solder coverage, solder bridges, lifted leads, tombstoning, and visible foreign material.
The selected product class must be identified before the inspection program is released. IPC-A-610 distinguishes Class 1, Class 2, and Class 3 acceptance expectations. A feature accepted for one class can require review or rejection for another. An AOI threshold that is appropriate for a general commercial assembly may be too permissive for a high-reliability product, while a Class 3 threshold applied without supporting process capability can generate excessive false calls and unnecessary handling of sound assemblies.
IPC J-STD-001, Requirements for Soldered Electrical and Electronic Assemblies, provides the process-oriented companion reference. AOI cannot verify internal solder-joint wetting, metallurgical bond quality, or hidden barrel fill in a way that replaces other inspection methods. It can, however, detect visible evidence of conditions addressed by J-STD-001: insufficient solder at accessible terminations, disturbed joints, solder balls, bridging, damaged conductors, flux residue where prohibited by the assembly specification, or exposed component leads beyond the allowed condition.
The distinction matters when creating defect codes. A visible fillet shape is not automatically proof of an electrical or metallurgical defect. Conversely, an optically acceptable leaded joint can still contain a concealed void, head-in-pillow condition, or insufficient bottom-side attachment. AOI disposition rules should state when an optical finding is final, when it requires human review, and when it triggers X-ray, electrical test, microsection analysis, or process investigation.
AOI rules need a controlled source, not visual approximation
IPC documents establish general acceptance criteria, but a production-ready AOI program also needs controlled product-specific information. The assembly drawing, bill of materials, centroid data, fabrication data, component datasheets, approved sample board, and customer workmanship specification together define the inspection source. Where a product requirement is stricter than an IPC baseline, the product requirement governs. Where documentation is silent, the chosen IPC revision and class should be formally identified rather than assumed.
Component polarity is a common example. IPC-A-610 addresses marking and orientation conditions, yet AOI polarity logic depends on the actual package marking, silkscreen convention, CAD orientation, and approved library image. A diode marking hidden by adhesive, a laser mark with low contrast, or a reel change that alters package appearance can cause a correct component to be flagged as reversed. The remedy is not simply to widen polarity sensitivity; the library, component approval record, and image-reference conditions need review.
Placement inspection has a similar boundary. AOI measures offset and rotation relative to a programmed reference, but the acceptance decision should reflect pad geometry and solderable termination overlap rather than a generic positional number. A small passive component can appear shifted while retaining sufficient termination engagement. A fine-pitch lead may remain near its programmed coordinate yet sit on a damaged or contaminated pad. Inspection limits should therefore be tied to land pattern geometry, component termination dimensions, and the assembly acceptance requirement.
Visible defects versus process indicators
A well-designed inspection library separates conditions that require rejection from conditions that signal process drift. Treating every visual variation as a defect increases false-call volume and encourages repeated manual review. Treating every variation as cosmetic creates an escape path for soldering and placement problems.
For example, solder paste squeeze-out around a chip component may be acceptable when there is no bridge, no exposed termination condition, and no evidence of disturbance. Repeated squeeze-out at one panel location is still useful process information because it can indicate stencil blockage, support-pin pressure, board warpage, or placement-force variation. The AOI system should retain the image and defect classification even when the board is accepted, allowing the condition to be correlated with stencil cleaning, printer settings, placement equipment, or reflow profile records.
Tombstoning requires different treatment. It is normally an assembly defect because one termination is not properly soldered. Yet the optical signature can be confused with a component that is standing at an unusual angle due to shadowing or a damaged reference image. Multi-angle illumination and side-view capability improve detection, but library tuning must be validated on actual board finishes and component colors. Matte black packages, reflective nickel-gold surfaces, and tall adjacent parts each alter contrast.
Bridging criteria also need context. AOI is well suited to detect solder between gull-wing leads, chip terminations, and exposed pads. However, a dark region between leads may arise from flux residue, a camera shadow, conformal-coating edge effects, or a legitimate copper feature visible through a transparent solder mask. A rule based only on dark-pixel area produces unstable results. Reliable bridge detection combines expected lead geometry, solder-mask openings, lighting response, and verified defect images.
When AOI must be paired with another method
AOI is strongest at the stages where top-side or bottom-side surfaces are visible and repeatable. It should not be used as evidence for conditions that optical access cannot establish. Bottom-terminated components, ball-grid arrays, land-grid arrays, QFNs, and many connector terminations contain solder interfaces that are partly or fully hidden after reflow. X-ray inspection, electrical test, boundary-scan testing, functional test, or destructive analysis may be specified according to the product risk and accessible evidence.
Through-hole solder joints also illustrate the limitation. Top-side AOI can confirm component presence, orientation, lead protrusion, and obvious bridging. Bottom-side AOI can assess accessible fillet appearance. Neither view alone reliably establishes internal barrel fill, wetting through the plated-through hole, or copper damage within the hole wall. Criteria from J-STD-001 and the applicable assembly documentation should determine whether additional inspection or process validation is required.
Conformal coating introduces another inspection condition. AOI performed before coating has clearer access to solder joints and markings. AOI performed after coating may be needed to inspect coating coverage, bubbles, bridging, or masked areas, but the optical program must distinguish coating reflections from solder defects. Mixing pre-coating and post-coating images in one acceptance library is a frequent source of unstable thresholds unless the process stage is explicitly encoded in the inspection record.
Traceability and revision control
IPC-1782 is relevant when AOI findings must be connected to a traceable assembly history. The required traceability level varies by contractual, product, and risk requirements, but an AOI record is most useful when it can be linked to the board identifier, panel location, work order, lot, equipment program revision, component lot where applicable, inspection timestamp, reviewer disposition, and repair outcome.
Saving only a pass or fail result loses important evidence. A false-call rate rising after a lighting change, a new solder-mask finish, or a component-source substitution can reveal a measurement-system issue before it becomes a defect-escape issue. Conversely, a falling reject rate is not necessarily proof of improvement if the inspection threshold was loosened or a defect code was reassigned. Program revision history is needed to interpret trends correctly.
Each released AOI recipe should identify the governing IPC-A-610 and J-STD-001 revisions, product class, board revision, component-library revision, approved golden images, and exception rules. Engineering changes affecting pad layout, component body size, package marking, solder-mask opening, or polarity notation require a review of relevant AOI checks. Reusing an earlier recipe without that review can lead to a technically valid program inspecting the wrong physical condition.
Validating the inspection system
AOI validation should test the inspection method against known acceptable and known nonconforming conditions, not only against a nominal golden board. A clean reference board establishes alignment and appearance, but it does not demonstrate that the program distinguishes a marginal placement from a rejectable placement, or a true bridge from harmless residue.
- Defect samples should cover the actual package range, including fine-pitch leads, small chip components, polarized devices, connectors, and parts affected by glare or shadow.
- Inspection results need comparison with the governing acceptance criteria and, where applicable, an independent verification method. A machine classification alone is not the acceptance authority.
- Repeatability matters after changes to lighting, camera calibration, board support, conveyor settings, software version, or component source. These changes alter the image even when the assembly process is unchanged.
- False calls should be categorized by cause. A polarity false call caused by an unclear marking requires a different corrective action from one caused by incorrect CAD rotation data.
Measurement-system behavior deserves attention when AOI thresholds are close to the intended acceptance limit. Board warpage, fiducial damage, panel stretch, poor conveyor support, and inconsistent board registration can make a stable assembly appear shifted. The resulting image may be repeatable at one inspection station and unstable at another. Before changing placement limits, confirm alignment performance and physical support conditions.
Using ISO 9001 correctly in an AOI program
ISO 9001 is often cited alongside IPC requirements, but its role is different. It supports a controlled quality-management framework for documented procedures, competence, calibration or verification of monitoring resources where applicable, nonconforming-output control, corrective action, and retained records. It does not state the allowable solder bridge size, component offset, or lead condition for a particular PCB assembly.
An AOI procedure aligned with a controlled quality system should define program approval, access control, inspection-stage identification, alarm handling, review authority, defect coding, repair verification, and records retention. The procedure should also prevent a board from bypassing required inspection after rework. A repaired location may need reinspection under the same product-class criteria, while the repair record preserves the original finding and final disposition.
The practical standard set is therefore clear: use IPC-A-610 for visible assembly acceptance, use J-STD-001 for soldered-assembly requirements and process context, apply IPC-1782 when traceable inspection history is required, and use ISO 9001 to control the system that creates, approves, executes, and records the inspection activity. AOI delivers reliable quality evidence only when those references are translated into product-specific, validated, revision-controlled inspection rules.
Recommended News
- AOI TestingHow to verify ISO 9001 certification when sourcing electronicsISO 9001 certification electronics: learn how to validate certificates, audit scope and accreditation, and reduce quality risks when sourcing PCBs, EMS, and components.
- AOI TestingHow to verify a UL certified PCB assembly before production approvalUL certified PCB assembly verification made practical: review PCB markings, materials, components, traceability, and safety controls before production approval.
- AOI TestingHow to qualify an AOI inspection supplier for PCB defect detectionAOI inspection supplier qualification guide for reliable PCB defect detection. Learn how to validate detection accuracy, control false calls, assess traceability, and choose dependable support.
- AOI TestingHow to catch solder joint defects in through hole assembly testingThrough hole assembly testing: discover how visual inspection, electrical tests, X-ray, and process controls catch hidden solder joint defects before they cause costly failures.
- AOI TestingWhich AOI inspection standards apply to PCB assembly quality control?AOI inspection standards for PCB assembly: learn how IPC-A-610, J-STD-001, IPC-1782, and ISO 9001 guide defect criteria, traceability, validation, and reliable quality control.
- AOI TestingHow AOI testing supports electronics quality control in the USAElectronics quality control USA teams use AOI testing to catch visible PCB assembly defects early, improve traceability, and strengthen reliable production outcomes.